PRODUCT FAMILIES

Six families of vacuum chambers and components, built to drawing

These are the six families we build most often and get asked about first during drawing review. Each entry states only what we can confirm: material, forming, interfaces and how it is tested. Geometry, dimensions and tolerances are settled from your drawing.

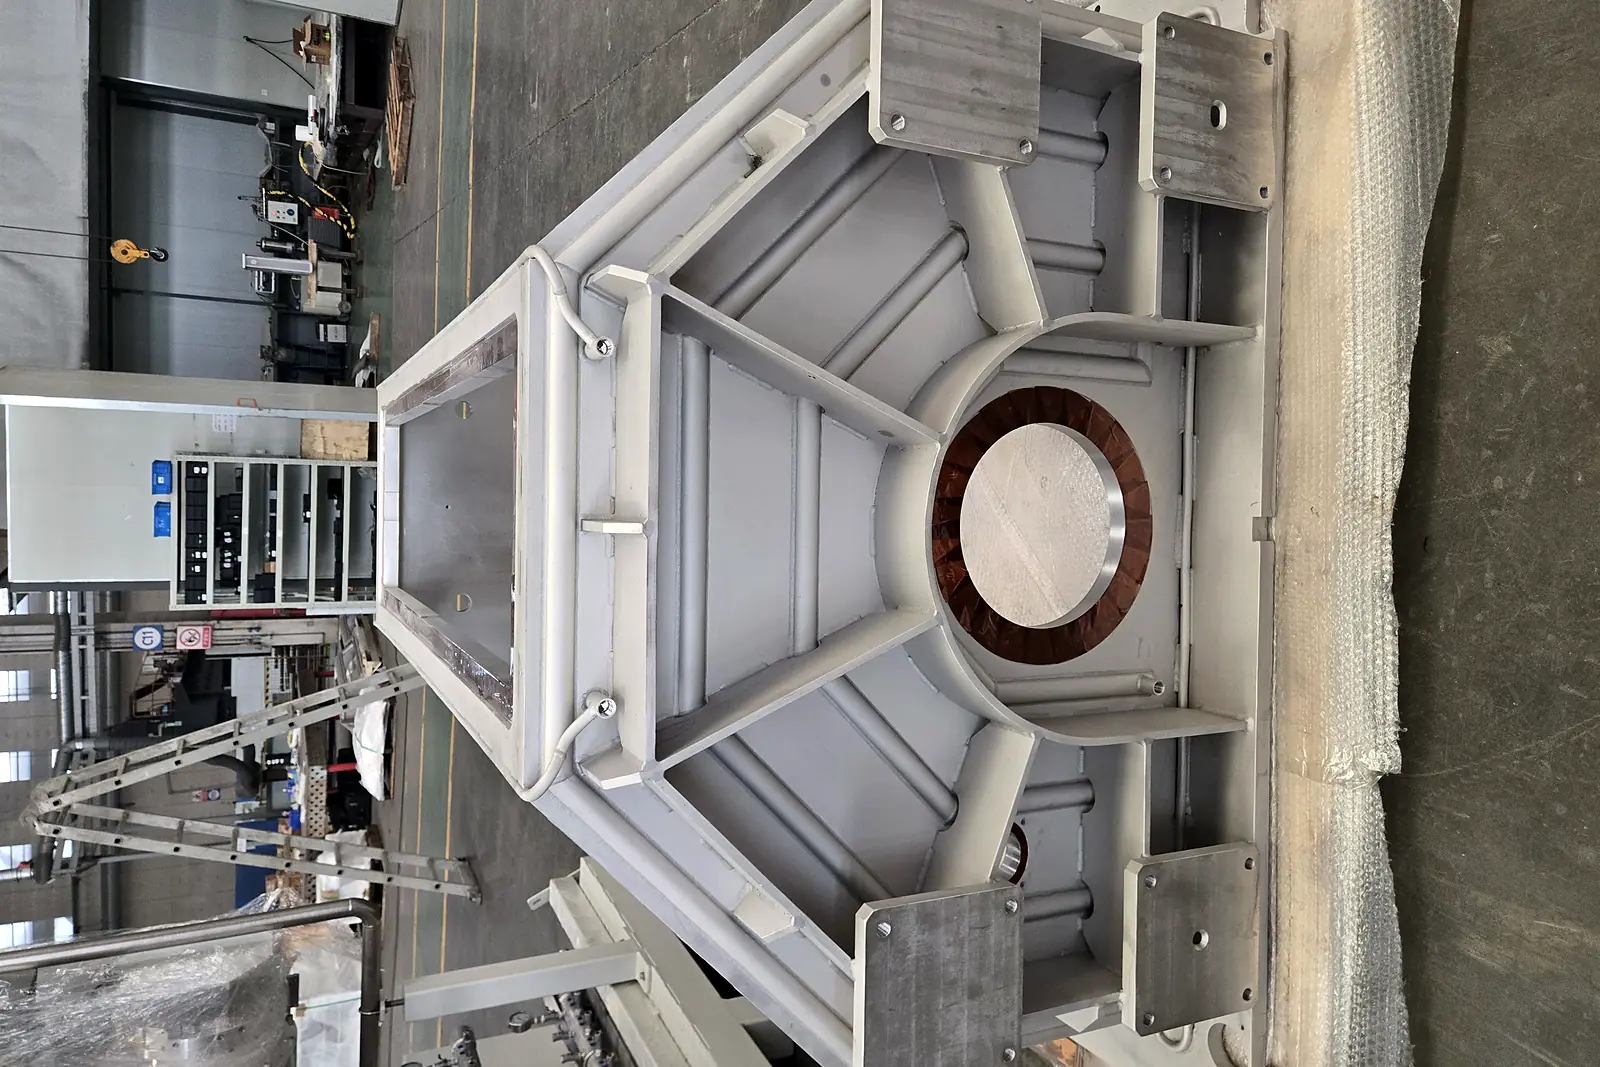
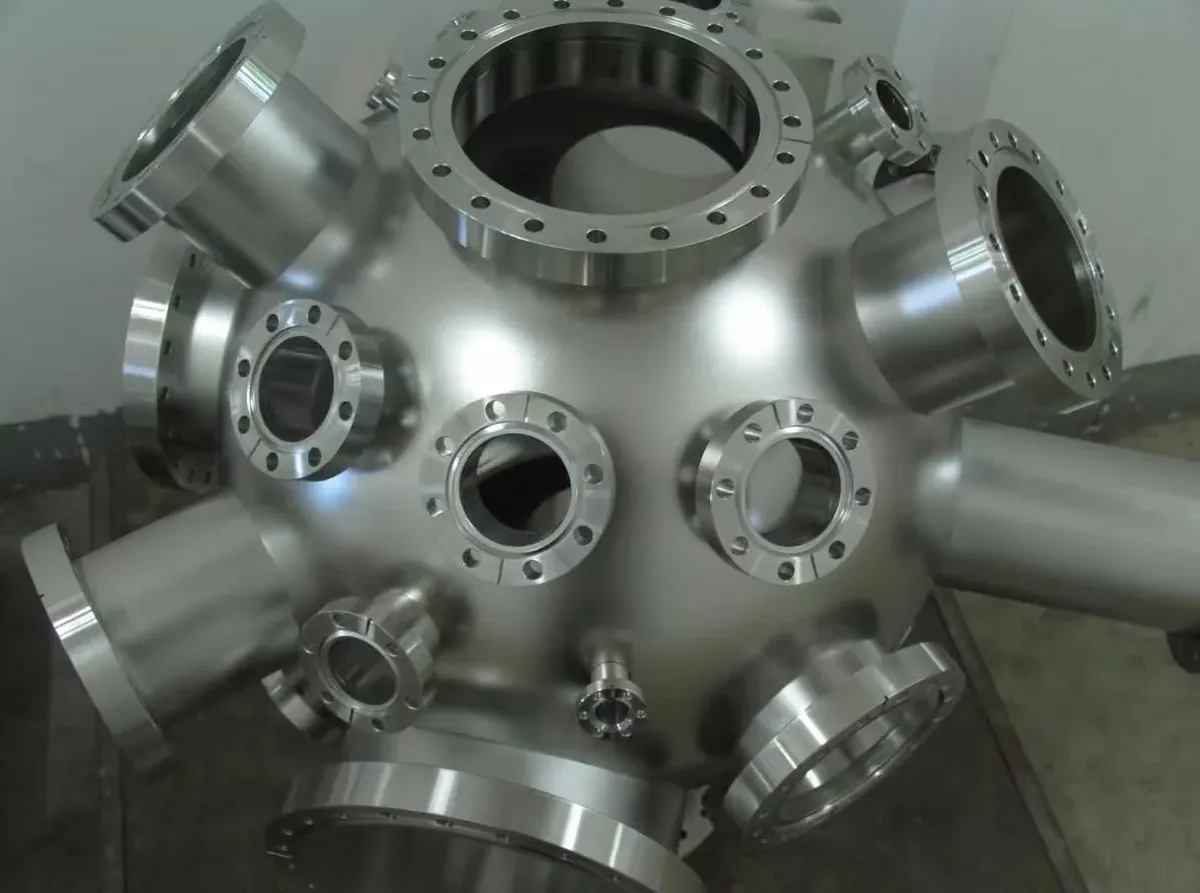
Cylindrical stainless steel vacuum chamber shell in the workshop

Cylindrical vacuum chambers

Shell rolling, flange fit-up and sealing-face machining happen in one plant, so long seams are not split across suppliers.

  • Material: 304 / 304L / 316L stainless, to the drawing's grade and surface requirement
  • Forming: 30 kW laser blanking, 400 t / 6.2 m press brake and rolling; multi-tonne units handled by the 50 t crane
  • Interfaces and testing: flanges, viewports and feedthroughs per drawing; every unit helium tested in the 1×10⁻⁹ Pa·m³/s range
See this family in detail →
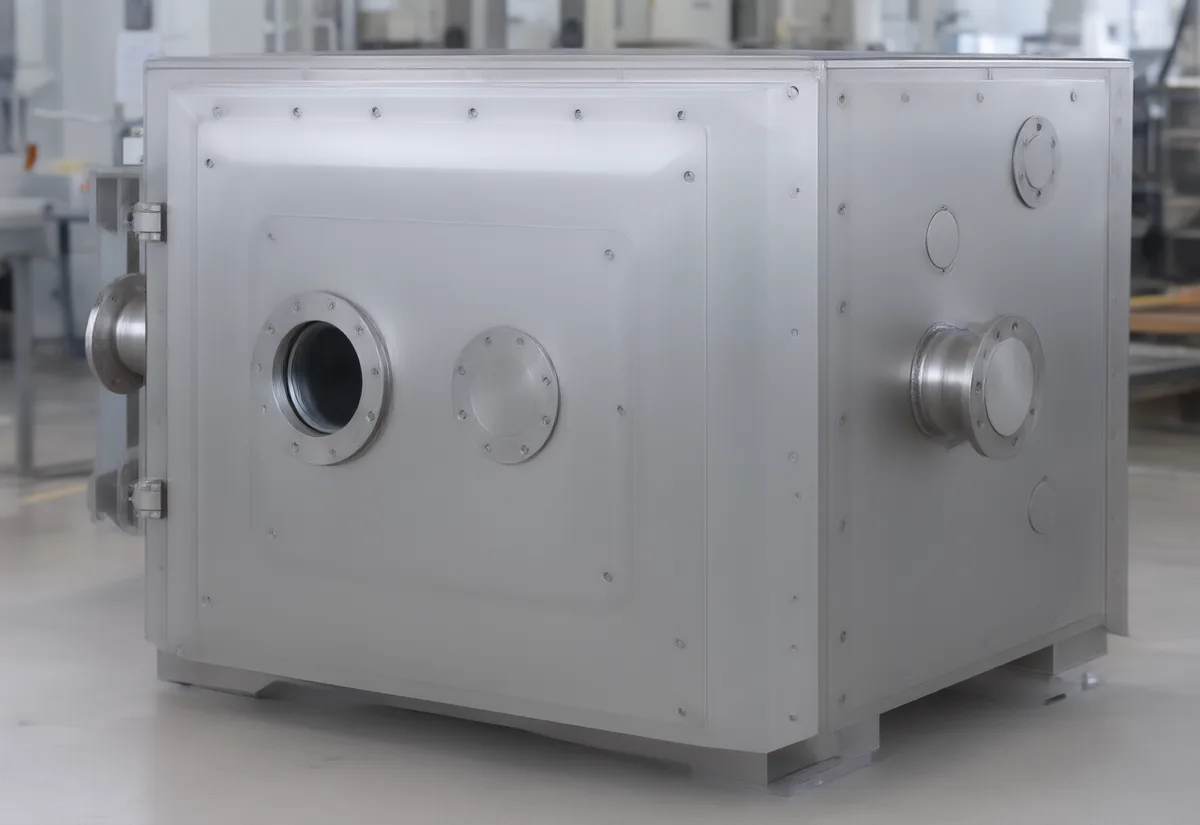
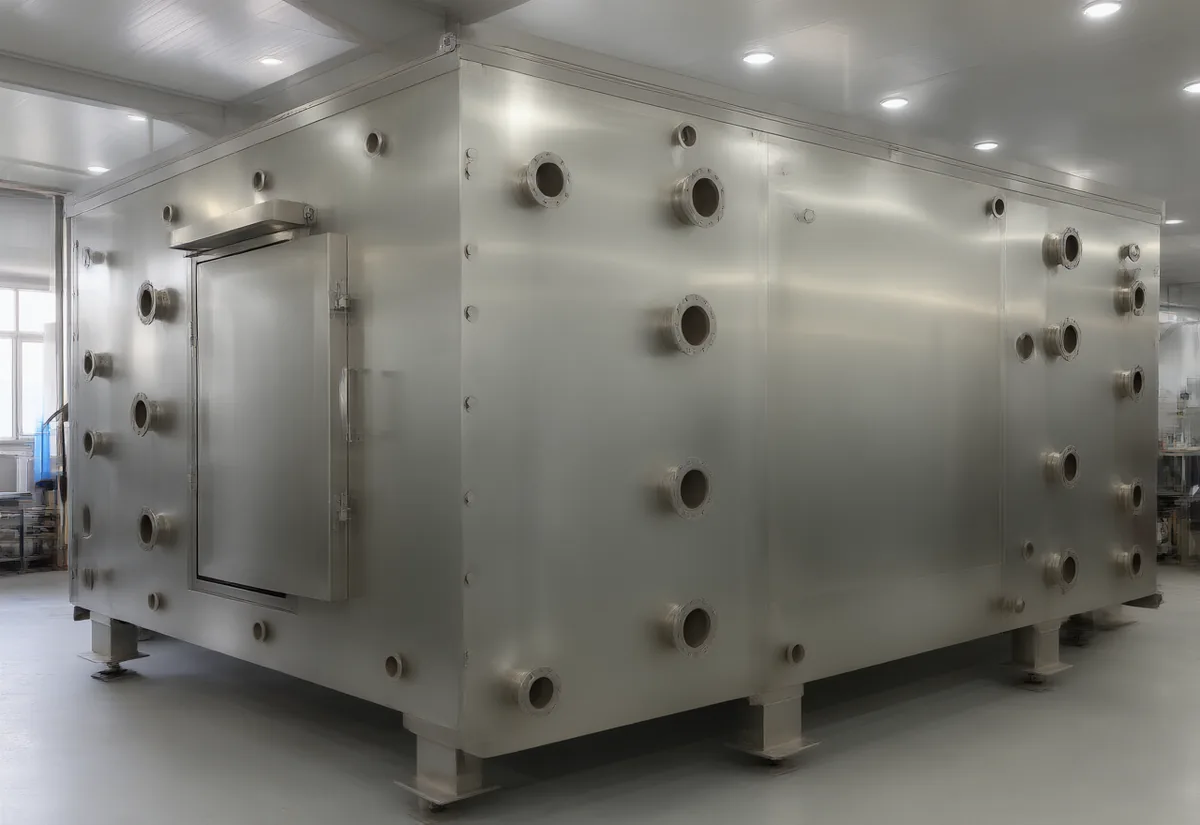
Square stainless steel vacuum chamber with a hinged door

Square and box chambers

Large sheets formed in one bend, door frames and hinged doors fitted to the drawing — geometry follows the drawing, not a catalogue.

  • Material: mainly 304L sheet, grade and thickness per drawing
  • Forming: sheets up to the 6.2 m bend length formed in one operation, reducing weld seams and re-straightening
  • Interfaces and testing: door frames, seal grooves, viewports and ports per drawing; leak tested per unit, dimensions recorded to the agreed scope
See this family in detail →
Multi-tonne 304L horizontal vacuum chamber

Large horizontal and multi-tonne chambers

Chambers weighing several tonnes and metres long, assembled and turned as one piece under the crane.

  • Unit weight: multi-tonne, lifted and rotated as one piece by the 50 t crane rather than split for shipment
  • Structure: the split strategy and lifting points for long chambers are settled during drawing review
  • Testing and dispatch: leak tested as a whole, then crated to the export packing requirement with records inside
See this family in detail →
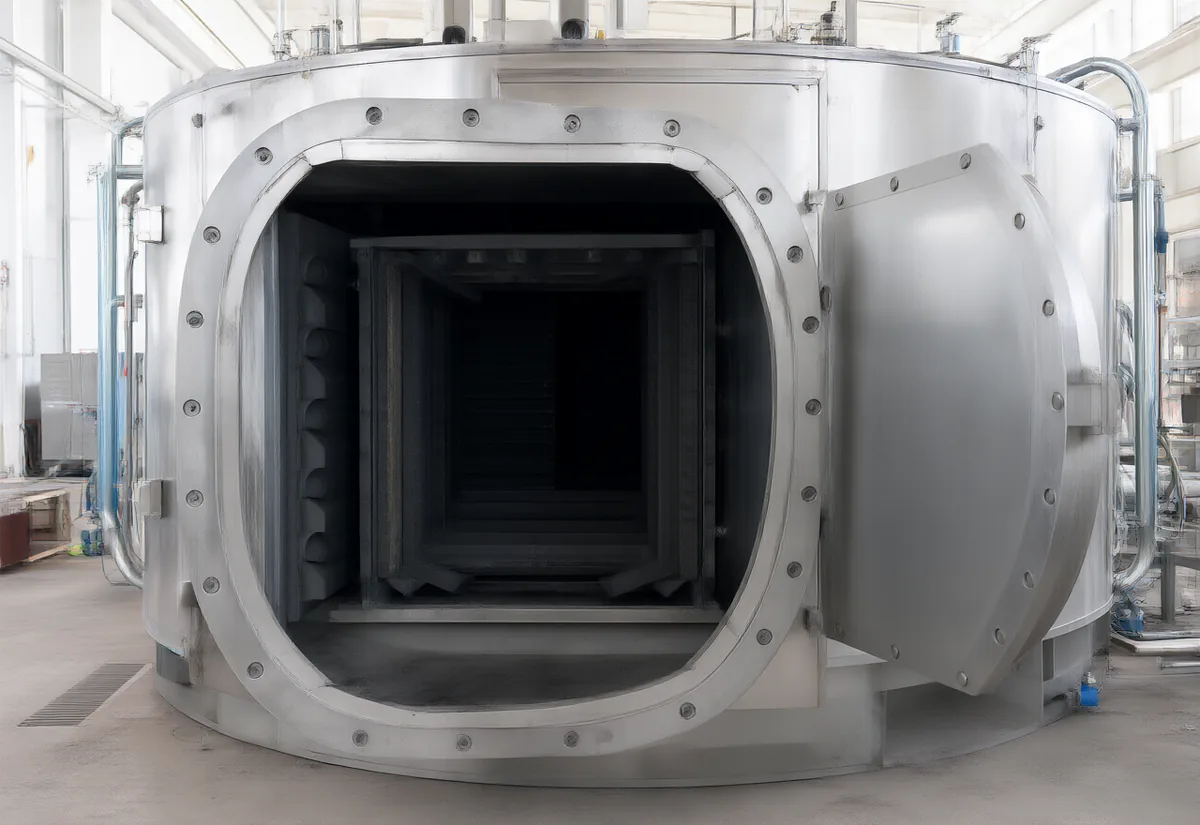
Vacuum heat-treatment furnace chamber with its door open

Vacuum furnace and heat-treatment chambers

Furnace shells, doors and cooling-water interfaces built to drawing, with heating-element and insulation fits agreed at review.

  • Structure: shell, door, flanges and lifting lugs to drawing; sealing faces fitted against the door frame
  • Interfaces: positions for heating elements, insulation, thermocouples and water lines agreed per drawing, with openings confirmed before welding
  • Testing: helium leak testing after welding; the scope of water-circuit and gas-line tests is agreed for the project
See this family in detail →
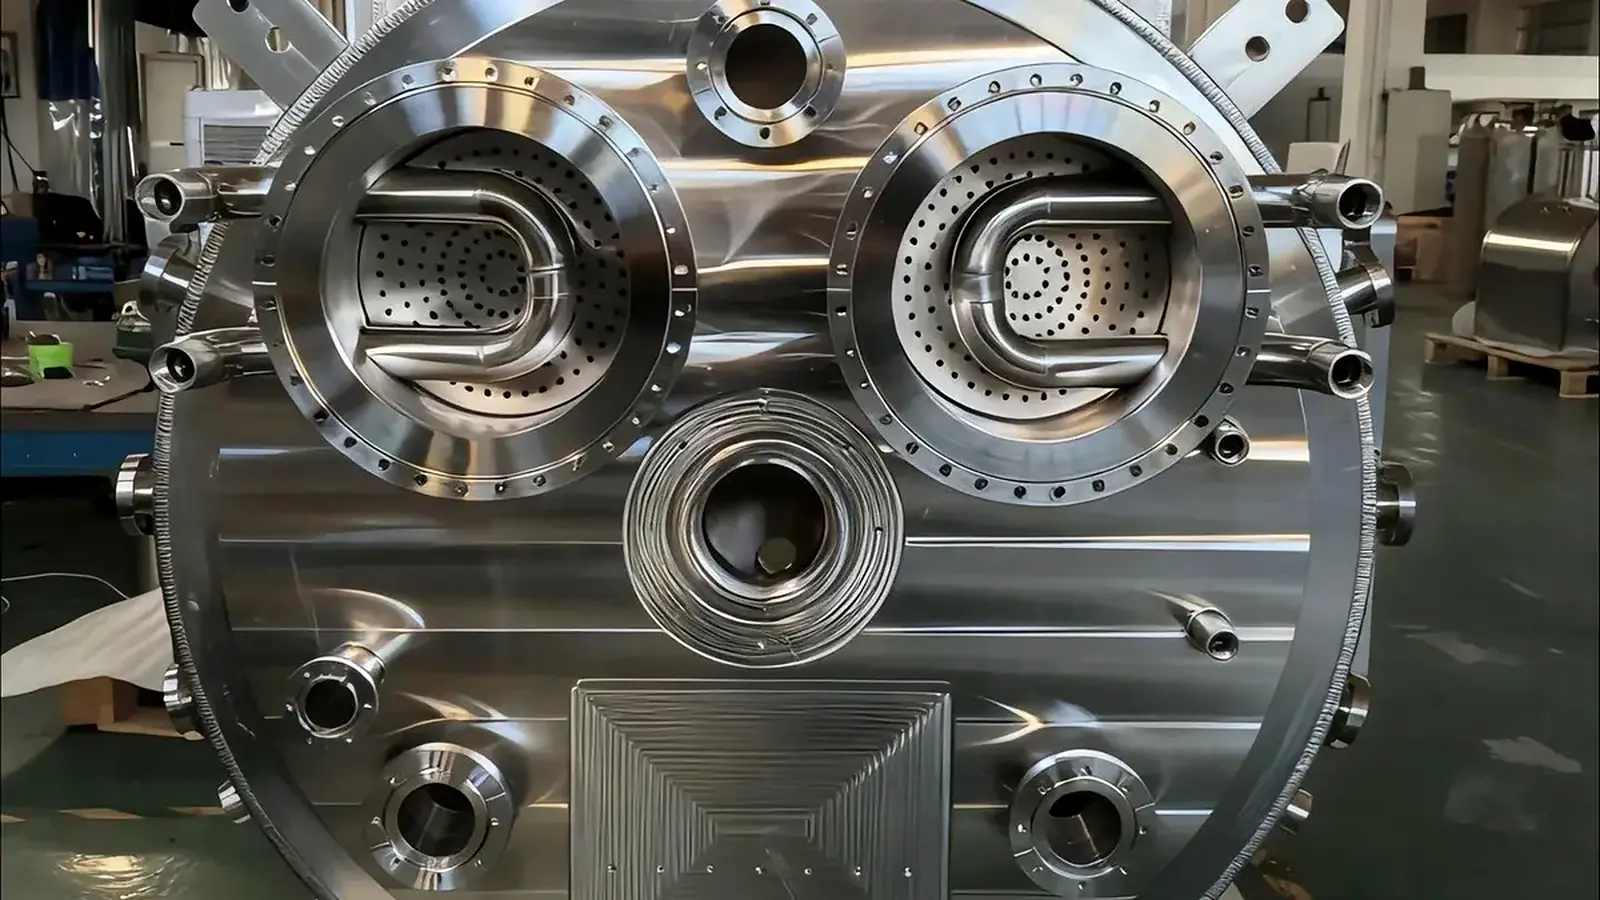
Vacuum coating process chamber with viewport and electrode feedthroughs

Coating and deposition process chambers

PVD, CVD and magnetron-sputtering chambers with target, gas-line and feedthrough interfaces laid out to drawing.

  • Structure: square or round process chamber; door, viewports, electrode feedthroughs and target ports per drawing
  • Manufacturing: welded inside the controlled clean welding environment, with the following surface steps scheduled in
  • Testing: helium leak tested per unit; particle and cleanliness requirements are agreed per project rather than quoted as a generic class
See this family in detail →
Stainless steel vacuum flanges and feedthrough assembly

Flanges, feedthroughs and sealing components

Flanges, feedthrough bodies and sealing faces machined to drawing, with critical fits recorded piece by piece.

  • Series: CF knife-edge, KF quick-release and ISO-K double-claw flanges, plus blanks, centring rings, adaptors and feedthrough bodies, sized to drawing or confirmed against the mating standard part
  • Machining: flanges, feedthrough bodies and sealing faces turned and milled to drawing, with fits controlled to the drawing; O-ring groove form and base to drawing, otherwise cross-checked against the mating part
  • Material: mainly stainless, grade and heat-treatment condition per drawing
  • Testing: critical dimensions recorded per piece; leak tested together with the chamber, with test conditions agreed at review
See this family in detail →

This page describes the range we can build, not a catalogue of models. PANO builds to drawing and does not sell standard chambers or complete systems, and we do not quote a base pressure for a chamber on its own — that depends on the pump set, seals and process, and is agreed per project.

From drawing to dispatch

Most enquiries move through four steps. The first one costs nothing and usually decides whether the rest is worth doing.

01Send a drawing or the basic dimensions

A PDF or STEP file is ideal. If there is no drawing yet, send the inner dimensions, material, port list and what the chamber will do.

02Drawing review and quotation

We come back on wall thickness, forming method, weld access, port positions and which inspection gates apply, then quote with those points written in.

03Cutting, forming and welding

Laser blanking, 6.2 m bending and rolling, then TIG and automated welding across 40-plus stations inside the controlled clean welding bay.

04Leak test, records and dispatch

Every chamber is helium tested, critical dimensions are recorded, and it is crated to the export packing requirement with records in the crate.

Send a drawing, get a priceSee how chambers are made and tested

WhatsApp us