ProductsFamily
Coating and deposition process chambers
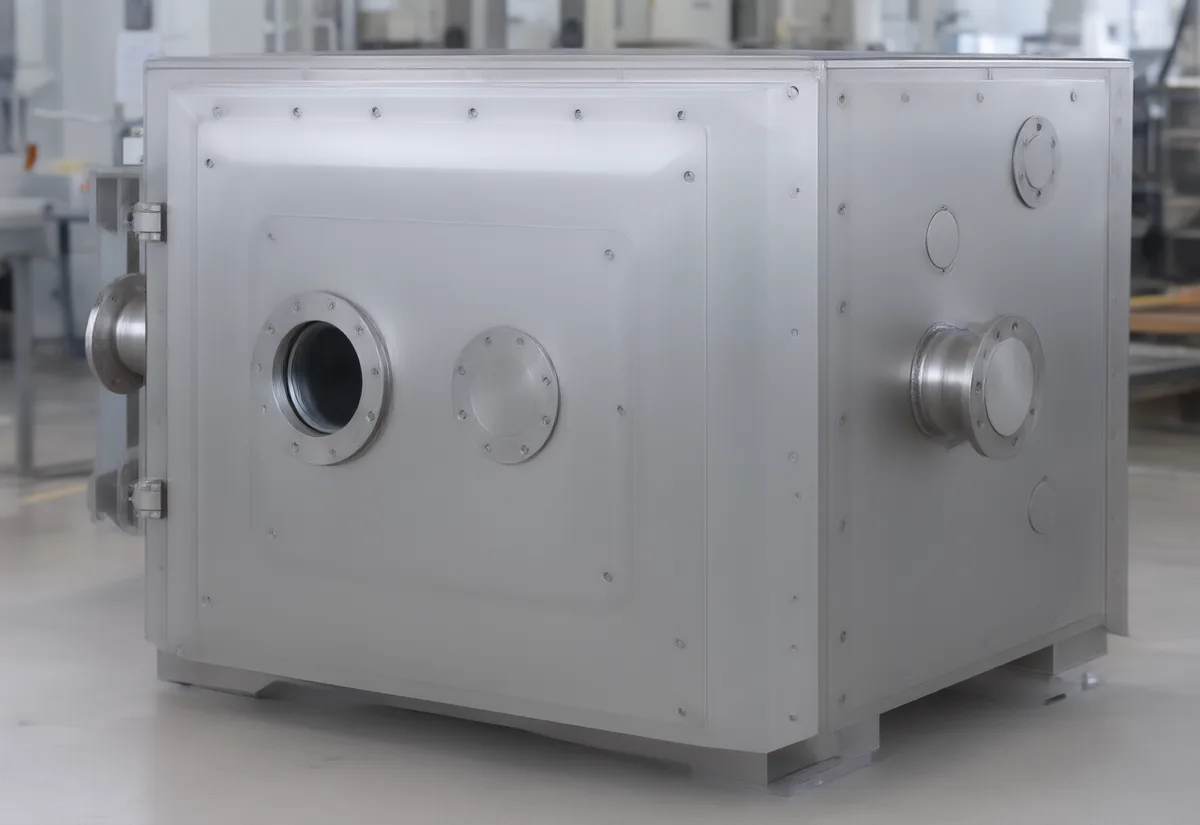
PVD, CVD and magnetron-sputtering chambers with target, gas-line and feedthrough interfaces laid out to drawing.
Half of a coating chamber is the vessel, the other half is targets, gas lines, feedthroughs and cleanliness. We build the chamber and the interface fits, weld inside the controlled clean welding environment, and take particle and cleanliness requirements from the project rather than quoting a generic class.
How it is built
The square or round process chamber is formed to drawing, with doors, viewports, target ports, electrode feedthroughs and gas inlets cut and welded to drawing; internal surfaces are finished to the process requirement (polished, electropolished or blasted, as marked). Welding happens inside the controlled clean welding environment, with post-weld cleaning and inter-stage protection to the agreed scope.
Interfaces and fits
Target spacing, feedthrough positions and gas routing are confirmed at review, because they have to line up with the power supply, gas cabinet and substrate holder. Blank flanges, viewports and sensor ports follow the drawing; anything unmarked is agreed at review.
How it is verified
Helium tested per unit; internal cleanliness checked by the agreed method (white-cloth wipe, visual, or your own standard), with particle requirements written into the project scope instead of a generic class on a web page. Internal surfaces are sealed before packing so transport does not contaminate them.
Technical summary
The table states the range we can confirm; dimensions, tolerances, thickness and flange standards are settled at drawing review.
| Material | 304 / 304L / 316L stainless, to drawing |
|---|---|
| Structure | Square or round chamber; doors, viewports, targets, feedthroughs and gas ports to drawing |
| Surface | Internal polish, electropolish or blasting per process requirement (marked on drawing) |
| Welding | Inside the controlled clean welding environment, with inter-stage protection as agreed |
| Testing | Helium leak test per unit; cleanliness checked by the agreed method, particle limits per project |
| Packing | Internal surfaces sealed before crating to avoid transport contamination |
What buyers ask
Can you guarantee a cleanliness class?
Not as a generic class. Give us the method — white-cloth wipe with visual judgement, particle counting, or your own company standard — and we test to it with the method written into the contract. If there is no method yet, we define one at review.
Can target and feedthrough positions still change?
Yes at review, before the drawing is frozen. After the ports are cut and welded, changes get expensive, which is why we insist on freezing those dimensions at review.
How fine can internal surface finishing go?
Polishing, electropolishing or blasting as the drawing requires, with roughness per the drawing callout; for tighter values we make a sample first and confirm before the batch.